Precision CNC machining built for complex programs.
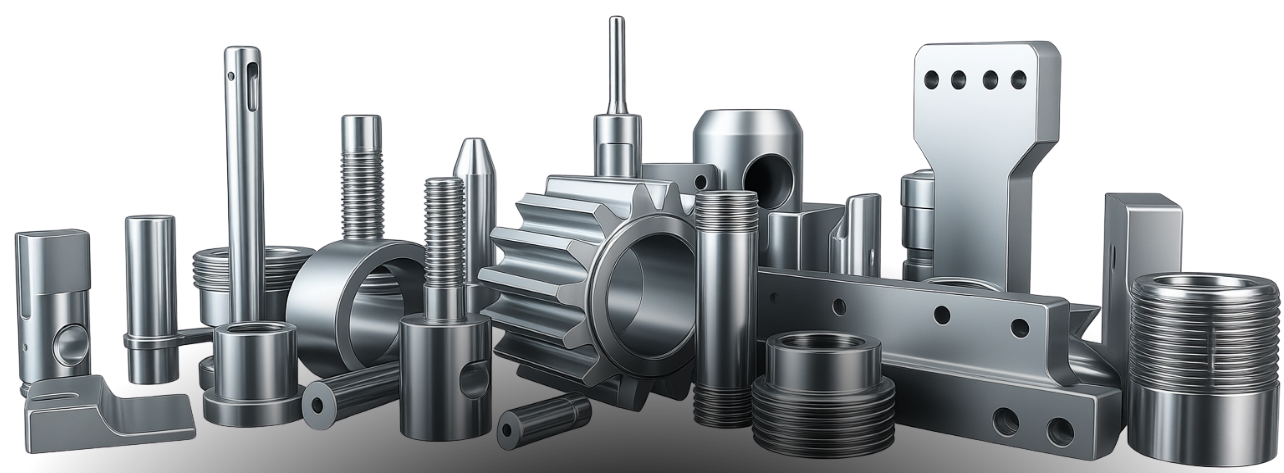
We coordinate precision CNC machining services across 3, 4, and 5-axis milling, CNC turning, Swiss machining, and wire EDM. Aluminum, stainless, titanium, Inconel, PEEK, and other standard and exotic materials, from a single prototype to a full production run.
One contact coordinates the program from start to finish. The jobs that break down somewhere else get built here.
Choosing your CNC machining process.
Not every part belongs on the same machine. Here is how we match the process to the requirement
3-Axis CNC Milling
Cutting on X, Y, and Z axes. The standard method for flat and moderately complex geometry.
Fastest setup. Most economical for simple parts.
Right when: The geometry is simple to moderate and doesn’t need simultaneous multi-axis movement.
Common parts: Brackets. Plates. Housings. Straightforward prototypes.
4-Axis CNC Milling
Adds rotational movement around one axis, reaching features around a part without a second setup.
One setup instead of two. Fewer chances for misalignment.
Right when: The part has features on multiple faces or needs indexed rotation to hit them in one operation.
Common parts: Cylindrical parts with cross-features. Manifolds. Rotational brackets.
5-Axis CNC Machining
Simultaneous movement across five axes, cutting complex contours and undercuts in a single setup.
Built for contours a 3-axis machine can’t reach.
Right when: Geometry is complex, tolerances are tight, or multiple setups would introduce stack-up error.
Common parts: Aerospace structural components. Complex housings. Medical instrumentation.
CNC Turning
The part rotates against a cutting tool. The standard process for cylindrical geometry.
Best fit for shafts, bushings, and other round parts.
Right when: The part is round, or a rotational axis is its primary geometry.
Common parts: Shafts. Pins. Bushings. Fittings.
Swiss CNC Machining
A sliding headstock turning process built for long, slender parts held to tight tolerances without deflection.
Tolerances to ±0.001″ through our vetted network. Where standard turning can’t hold the line.
Right when: The part has a small diameter relative to its length and needs to hold tolerance through the full cut.
Common parts: Medical device components. Connectors. Small precision pins and fasteners.
Wire EDM Machining
A thin, electrically charged wire erodes material to cut profiles too fine or too hard for a conventional cutting tool.
No cutting force. The only option for hardened tool steel and fine internal features.
Right when: The material is hardened or exotic, or the feature (a slot, keyway, or sharp internal corner) can’t be reached with standard tooling.
Common parts: Hardened tooling components. Fine internal features. Exotic alloy parts.
CNC Machining Specifications.
Whichever process fits your part, here’s what to expect. If your specs fall outside these, send the drawings anyway. The jobs other suppliers turn down are often the ones we do best.
- Tolerances
- ±0.005" standard · Tighter tolerances reviewed during quoting
- Minimum part size
- 0.25" x 0.25" x 0.25"
- Maximum part size
- 72" x 72" x 28"
- Metals
- Aluminum · Steel · Stainless steel · Titanium · Inconel · Copper · Brass
- Plastics
- ABS · POM (Delrin) · PEEK · Nylon · UHMWPE · Most engineering plastics
- File formats
- STEP, IGES, GD&T, native CAD, 2D prints
- Quote turnaround
- Within 24 hours
- Quality
- ISO 9001:2015 · AS9100 compliant · Engineer review before production · Inspection before shipment
Tolerances don’t get more forgiving under pressure.
Neither do we.
Common questions about CNC machining
A few things engineers and buyers ask before sending us a drawing.
Tight tolerances are available through our vetted vendor network, down to ±0.001″ on critical features. We flag which dimensions actually need that level of control during engineer review, since applying the tightest callout to an entire part instead of the two or three features that require it drives up cost without adding value.
Our network machines aluminum, steel, stainless steel, titanium, Inconel, copper, and brass, plus engineering plastics including PEEK, Delrin, nylon, and UHMWPE. That covers 3, 4, and 5-axis CNC milling, turning, Swiss machining, and wire EDM. If a material is unusual or hard to source, that’s exactly the kind of conversation a single point of contact is built for.
Yes. Our vendor network machines titanium and Inconel across 3, 4, and 5-axis CNC milling, turning, and wire EDM, from single prototypes to production runs. Both alloys are hard on tooling and generate heat that can affect tolerances, so every program goes through engineer review before it reaches the shop floor, and we route it to a vendor with proven experience in that specific alloy. Standard tolerances are ±0.005″, with tighter callouts down to ±0.001″ on critical features. These materials show up most often in aerospace, defense, and medical programs, which is why AS9100 and ITAR requirements are handled within the same network.
A real person reviews your files and reaches out within 24 hours. Simple parts move quickly. Complex prints with GD&T, multiple setups, or tight tolerances may need a quick clarifying question before a full quote goes out.
Yes, from a single machined prototype through production volumes, with the same engineer review and point of contact at every quantity.
Yes. AS9100 Compliant, ITAR Registered, and NIST 800-171 Compliant standards apply across the vendor network for programs that require them.
A portal matches your file to whichever vendor bids fastest. We match your project to the vendor in our network that’s equipped to run it well, with engineer review before it ever reaches the shop floor and one contact who owns it through delivery.
Trusted Across Critical Industries
Precision and reliability aren’t optional in these industries. Neither is our commitment to both.
Send us your files.
A real person will contact you within 24 hours.