Every internal or external corner on a CNC machined part needs a decision: fillet or chamfer. It looks cosmetic, and it affects machining time, tool selection, stress performance, and how the part mates with whatever it bolts, presses, or slides into. Get it wrong and you’re either paying for a feature your part doesn’t need or leaving a stress riser in a spot that’s going to crack under load. Here’s how to make the call.
What each one is
A chamfer is a flat, angled cut across an edge, usually 45 degrees though not always. A fillet is a rounded, radiused transition between two surfaces. They look similar at a glance. Mechanically and in the machine, they behave very differently.
Machining time and tooling
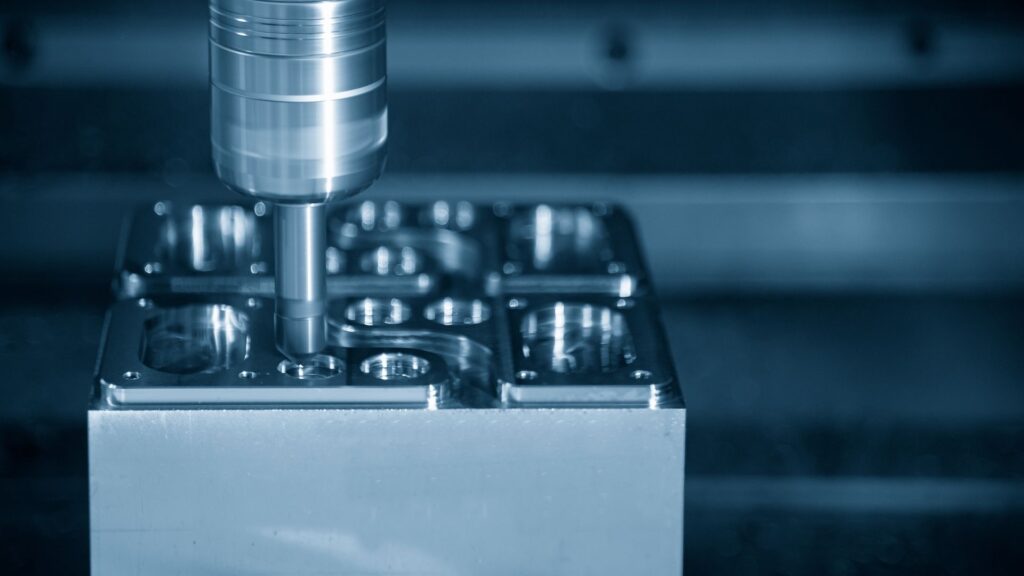
Chamfers are typically the faster, cheaper feature to cut. A chamfer tool or the cutter’s own lead angle can knock one out in a single pass on most CNC machines. Fillets, especially internal ones, need a ball-nose or corner-radius tool matched to the radius specified, and internal fillets are limited by the smallest tool that can physically reach into the corner. Specify a tighter internal radius than the smallest practical tool allows and our vetted vendor network will flag it before it gets cut, because it usually means a redesign. Sharp inside corners are one of the drawing callouts that raise your quote.
Stress and fatigue performance
This is where the decision stops being about cost. A sharp internal corner concentrates stress. A chamfer turns that corner into two sharp transitions, which doesn’t solve the problem. A fillet spreads the load across a smooth radius, which is why fatigue-loaded parts like brackets, structural components, and anything that sees repeated load cycles almost always call for a fillet at internal corners. If your part will see vibration or cyclic loading, don’t default to whatever’s faster to draw.
Assembly and function
Chamfers earn their keep on mating features. A chamfered edge on a shaft, a hole, or a fastener location makes assembly easier, guides parts into alignment, and removes the sharp edge that would otherwise catch on an O-ring or gasket during insertion. Fillets don’t do this job as well, because their rounded profile doesn’t provide the same lead-in geometry. On turned parts, the same logic applies to thread starts and shoulders, covered in our design rules for CNC turned parts.
The practical rule
Default to chamfers for edges that need to deburr cleanly, ease assembly, or don’t carry significant load. Default to fillets for internal corners on load-bearing or fatigue-sensitive features, and check your fillet radius against realistic tooling before it goes out for quote. When you’re not sure which one your part needs, ask before the design gets locked, rather than after the first article comes back. The CNC machining design guide lists recommended radii and other edge rules.
Send us the drawings and our team will flag any edge treatment that’s going to cause a problem in the shop before it costs you a re-quote.
Frequently asked questions
Chamfers are usually cheaper. They can often be cut in a single pass with a standard chamfer tool, while fillets need a tool matched to the specified radius.
For internal corners under load, a fillet. It spreads stress across a smooth radius instead of concentrating it at sharp transitions, which improves fatigue life.
It’s set by the smallest end mill that can reach the corner at the required depth. Deep pockets need larger radii. Specifying a radius slightly larger than the tool lets the cutter move smoothly through the corner.
On external edges that need deburring, on holes and shafts that need a lead-in for assembly, and anywhere a seal or gasket slides past an edge.