Every custom part eventually asks the same question: is this design ready to go from prototype to production, or is it still changing? Making that call too early locks in tooling costs against a design that isn’t finished. Making it too late means paying prototype-process pricing and lead times for parts you should already be running at volume. Neither mistake shows up on the invoice for the part in front of you. Both show up in the total program cost.
There’s no universal volume number that triggers the switch. The right moment depends on how stable the design is, as much as how many units you need next quarter.
What actually changes at the prototype to production transition
Prototype and production can be entirely different processes. Depending on the part, the transition can mean:
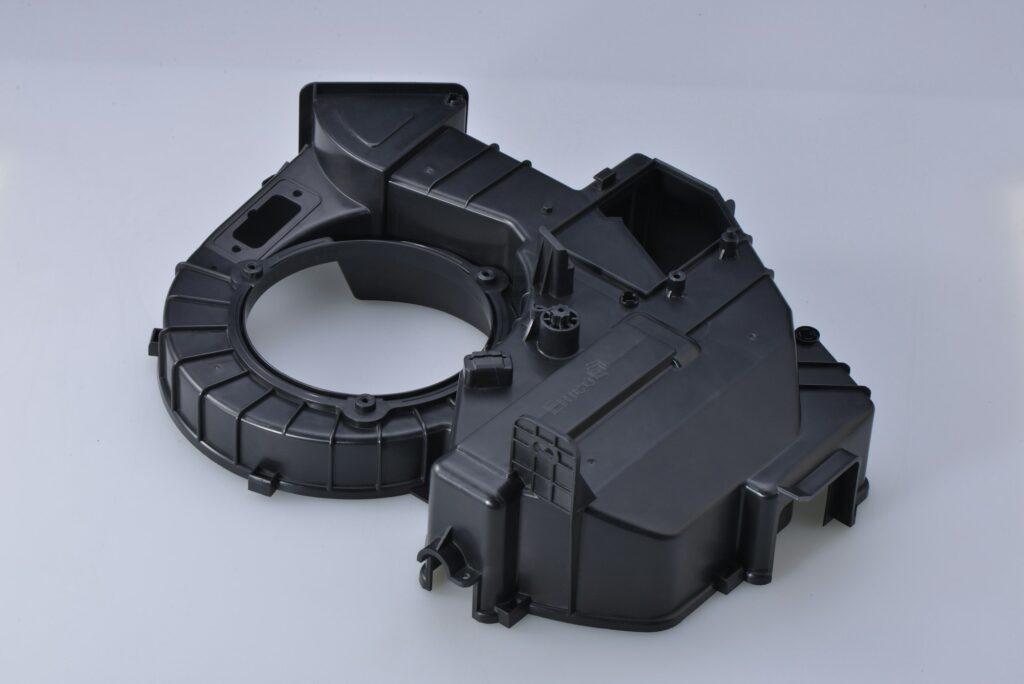
- 3D printed or CNC machined prototypes moving to injection molded production parts
- Soft or bridge tooling moving to hardened, production-grade tooling
- Manual or low-rate assembly moving to a repeatable, documented build process
- One-off material certifications moving to a qualified, traceable material supply chain
Each of those shifts changes the cost structure. Tooling is a fixed cost paid once and amortized across the run. Prototype processes carry no tooling cost but a much higher per-part price. Committing to tooling before the design is locked means paying for changes twice, once in engineering time and once in tooling rework. Our breakdown of what drives mold cost covers where that money goes.
Signals a design is ready for production tooling
- The design has been through at least one full manufacturability review, beyond a fit-check prototype run
- Critical dimensions and tolerances are called out deliberately rather than inherited from a CAD default
- Material has been qualified for the application rather than picked for prototype convenience
- Volume projections are stable enough to justify a fixed tooling investment
- The last round of prototype iterations changed cosmetic or minor details, leaving core geometry and function alone
If a design is still absorbing structural changes between revisions, it isn’t ready for hard tooling yet, however close the launch date is. That pressure to commit early is where programs end up paying for a mold change six weeks after cutting steel.
The cost of switching too early
Production tooling is built around a frozen geometry. A design change after tooling is cut costs more than the tooling modification. It costs the schedule slip while the tool is reworked, the scrapped parts already run against the old geometry, and in some cases a full requalification if the change touches a critical dimension. On regulated programs, that requalification carries its own paperwork and timeline.
The instinct to lock in production early usually comes from a launch date rather than design readiness. A launch date doesn’t change how many more revisions the design needs.
The cost of waiting too long
The opposite mistake is just as real. Running production volume through a prototype process means paying a per-part premium indefinitely, absorbing longer per-unit lead times as orders scale, and living with the wider process variation that comes with lower-volume methods. A part that’s been stable for three prototype rounds with no design changes is likely costing more than it needs to, every week it stays on a prototype process.
This is where a program benefits from a partner tracking both sides of that curve. Precision Expedited’s project managers flag when a part has outgrown its current process and when tooling for injection molding, or a shift to production machining runs, pencils out against the volume ahead. The process capability sits with our vetted vendor network, matched to the part and volume. For quantities still in the 1 to 100 range, our guide to choosing a prototype process by quantity is the better starting point.
Questions to answer before committing to production tooling
- Has this design gone through a formal DFM review, or only informal prototype feedback?
- What changed in the last two prototype revisions, and was it cosmetic or structural?
- Is the volume projection based on a firm forecast or an early estimate?
- Does the material and finish spec match what will ship, beyond what was convenient to prototype with?
- What’s the cost of being wrong in each direction, tooling paid too soon versus prototype pricing paid too long?
Frequently asked questions
Not a reliable one. Volume matters, but a design that’s still changing shouldn’t move to hard tooling regardless of quantity. Design stability is the better gate to check first.
Bridge tooling costs more per part than a full production tool but far less than a design change after hard tooling is cut. For a design that’s close but not fully proven at volume, it’s often the lower-risk path.
It’s uncommon and rarely economical once tooling is amortized, which is why the switch deserves a real design-readiness check before it happens.