Most CNC machining starts with 3-axis: the tool moves in X, Y, and Z. For a lot of parts, that’s exactly what’s needed. When geometry gets complex, though, 3-axis starts forcing compromises that cost time, money, and sometimes tolerance. Knowing when to move to 5-axis is a program cost and quality decision as much as a technical one.
What 3-axis machining does well
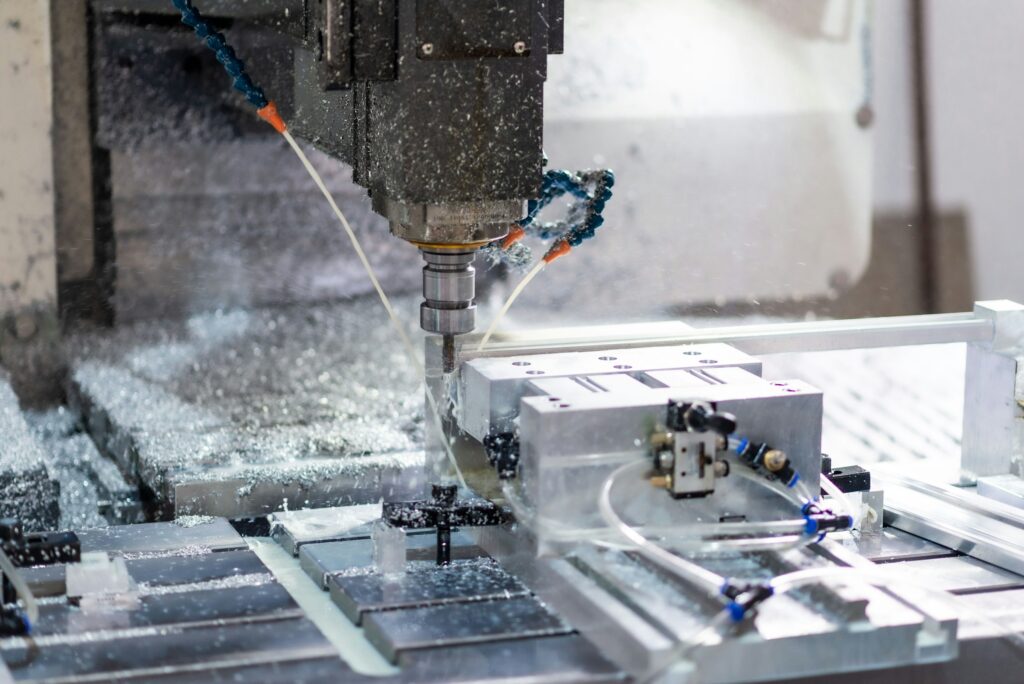
3-axis machining covers the majority of precision parts: prismatic parts with features reachable from one direction, flat surfaces, simple pockets, and straightforward bore patterns. It’s fast to set up, widely available across supplier networks, and well understood. For parts with simple geometry and tolerances around ±0.005″ or looser, 3-axis is usually the right answer. Adding axes to a part that doesn’t need them adds cost without adding value.
Where 3-axis hits its limits
The challenge with 3-axis is access. When a part has features on several faces, angled surfaces, or undercuts, the machine can’t reach them in one setup. That means repositioning the part, adding fixturing, and stacking tolerances across operations. Every repositioning introduces a chance for error, so tight-tolerance parts with multi-face features run across several 3-axis setups carry real risk of tolerance drift.
What 4-axis and 5-axis add
4-axis machining adds rotation around one axis, so features around a cylindrical part can be cut without repositioning. It’s a meaningful step up for parts with radial features or circumferential patterns.
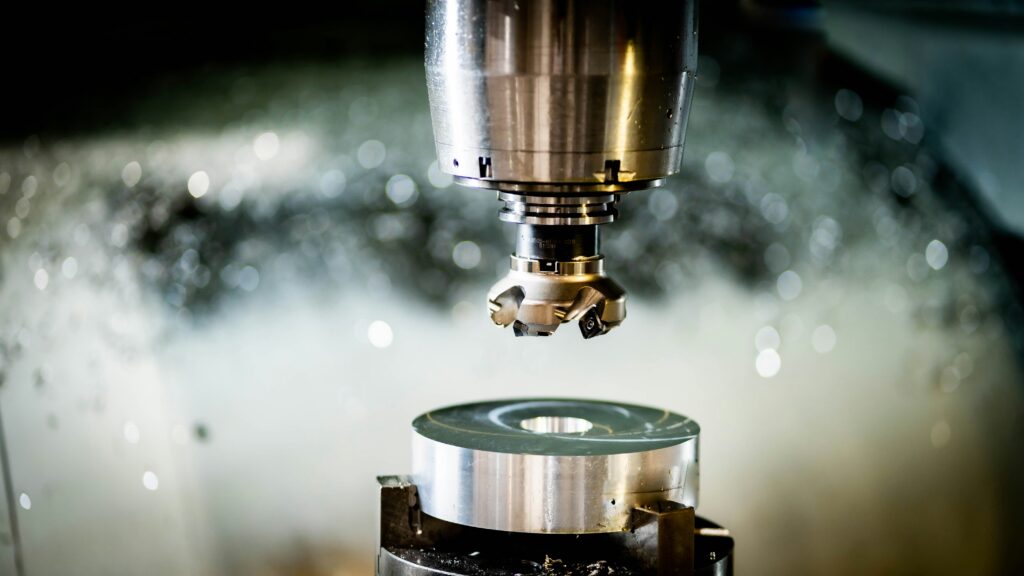
5-axis adds two rotational axes. The part or the tool can tilt and rotate, giving the cutter access to nearly any surface in a single setup. That matters for three reasons: complex contoured surfaces can be machined cleanly, fewer setups means less tolerance stack, and cycle times drop because tool paths are more efficient. Turned features follow their own rules, covered in design rules for lathe and Swiss work, and our guide to milling, turning, and EDM compares all the main processes.
Where 5-axis earns its cost
5-axis pays off on aerospace structural components with compound angles and tight tolerances, medical implant surfaces with complex contours, turbine and propulsion hardware, mold inserts with deep cavities and precise radii, and any part where single-setup, multi-face machining directly supports dimensional accuracy.
Precision Expedited’s vetted vendor network runs 3-, 4-, and 5-axis CNC machining plus EDM. The process gets matched to the part’s requirements rather than defaulted to whichever machine is open, and every drawing is reviewed before the job is placed so that decision gets made correctly upfront. If you’re not sure which approach fits, send us the drawings and we’ll give you a straight answer.
Frequently asked questions
The hourly rate is higher. On complex, multi-face parts the total cost can be lower, because one setup replaces several and scrap from tolerance stack drops.
When a part has features on several faces, compound angles, or contoured surfaces that need tight positional accuracy relative to each other.
3+2 positions the part at a fixed angle and then cuts with three axes. Full simultaneous 5-axis moves all axes during the cut, which is needed for continuous contoured surfaces like impellers and blades.